Bucket Elevators
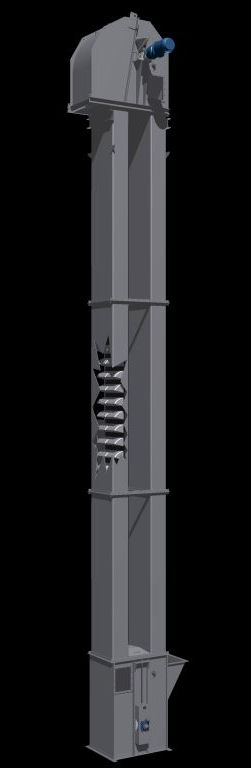
Bucket Elevators
We manufacture and design Bucket Elevator which is used to elevate or carry bulk raw material and grams in a vertical or from ground level to certain height and where continuous material flow is required. These are considered to be perfect for vertical displacement of bulk solids and other goods. Our design bucket elevators are based on the characteristics of the bulk material and the process requirements. The Bucket Elevator is constructed using stainless steel or mild steel buckets attached to a belt or chain. The belt can be made of natural fibres, rubber, plastic or metal.
Material is fed into an inlet hopper. Bulk materials are loaded into each bucket and conveyed it up to and over the head sprocket/pulley, then throwing the material out the discharge throat. The emptied buckets then continue back down to the boot to continue the cycle.
Our Bucket Elevators are utilized in many industries such as Sugar, Food, Grain, Fertilizer, Feeds, Rice, Flour, Cement, Coal, Foundry Sand, Wood and Chemical Industries.
Characteristics:
These are completely enclosed for dust and weather-tight operation
Low Power Consumption
High Efficiency
Max Height supplied 35 mtr & Max Capacity 100 TPH
Capacity: 40 Tons per Hour